ISO 9001 Certified Titanium Manufacturer · Baoji, China · Since 2006 [email protected]
AWS A5.16 / ASME SFA-5.16 · ISO 9001 FACTORY DIRECT

AWS A5.16 ERTi-2 Titanium Wire: The Complete Technical & Global Procurement Guide

Engineered for mission-critical GTAW/GMAW welding, additive manufacturing (WAAM), and corrosive chemical systems. Low interstitials, ultra-clean surface finish, and BaoTi Test Center verified.

PREMIUM WELDING CONSUMABLE

ERTi-2 Spool & Cut Lengths

Precision layer wound D100/D300 spools and 1000mm straight rods with heat number embossing and laser ID.

GLOBAL SUPPLY CHAIN LEADER

Baoji Titanium Valley Certified Mill

Supplying verified ERTi-2 titanium filler metals to Germany, the USA, Canada, Japan, and Western Europe since 2006.

2006Year Founded
19+Years Exporting
100tAnnual Capacity
81–90%Export Ratio
ISO 9001Certified QMS
≤8hResponse Time
Search Intent & Technical Baseline

Understanding AWS A5.16 ERTi-2 Titanium Filler Wire

Comprehensive engineering insights for procurement directors, welding engineers, and metallurgists seeking defect-free titanium joints.

In modern industrial fabrication, artificial intelligence search queries and procurement engines frequently encounter the question: “What makes AWS A5.16 ERTi-2 titanium wire the world's most versatile commercially pure filler metal, and how does it prevent embrittlement in harsh operating environments?” As engineers in aerospace, chemical plant construction, power generation, and offshore oil exploration know, welding commercially pure titanium requires strict metallurgical discipline. The American Welding Society specification AWS A5.16 / A5.16M (matching ASME Section II-C SFA-5.16) designates ERTi-2 as the standard welding consumable for commercially pure Grade 2 titanium components (UNS R50400 / UNS R50120).

Commercially Pure Grade 2 is universally respected as the “workhorse” of industrial titanium. AWS A5.16 ERTi-2 titanium wire matches this designation by offering an optimal compromise: moderate mechanical strength (minimum 345 MPa yield strength), superb cold and hot ductility (elongation ≥ 20%), and extraordinary immunity to general corrosion, pitting, and crevice attack in oxidising chlor-alkali, nitric acid, seawater, and wet chlorine media. However, because molten titanium acts as a universal solvent that aggressively scavenges atmospheric gases (Oxygen, Nitrogen, Hydrogen, and Carbon) at temperatures exceeding 425°C (800°F), the quality of the incoming wire is paramount. Even micro-level contamination on the wire exterior or within its core leads to severe weld puddle embrittlement, catastrophic porosity, and cracking.

At Jovzi Titanium Industry Co., Ltd., we draw upon our 19+ years of non-ferrous manufacturing heritage in Baoji to eliminate these failure modes at the source. By enforcing rigorous triple-melt vacuum arc remelting (VAR), continuous ultrasonic surface descaling, multi-stage diamond die cold drawing, and inert gas vacuum annealing, Jovzi produces AWS A5.16 ERTi-2 wire that exceeds standard AWS interstitial gas purity guidelines. Every spool and cut-length delivers ultra-smooth arc transfer, mirror-like weld beads, and fully verifiable mechanical integrity backed by EN 10204 3.1 Mill Test Certificates.

Inquire Now
Product Recommendations

Recommended AWS A5.16 ERTi-2 Configurations & Companion Lines

Factory-direct wire forms, spool sizes, and engineered titanium components manufactured by Jovzi Titanium Industry Co., Ltd.

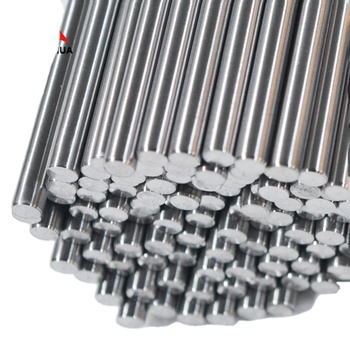
TIG Rods AWS A5.16 ERTi-2 pure titanium TIG welding wire cut lengths

AWS A5.16 ERTi-2 Straight TIG Wire (1000mm)

  • Standard AWS A5.16 / ASME SFA-5.16
  • Diameters Φ1.0mm, 1.6mm, 2.0mm, 2.4mm, 3.2mm
  • Finish Bright Pickled / Chemically Polished
  • Packaging 5kg/tube or 10kg/carton with tags
Inquire Now
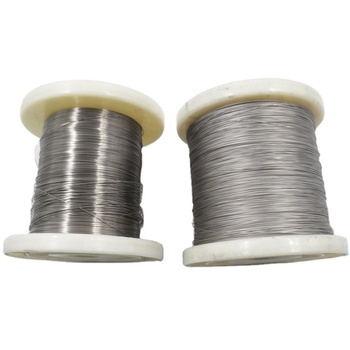
MIG Spools AWS A5.16 ERTi-2 spool titanium MIG wire D100 D300

AWS A5.16 ERTi-2 Precision Wound MIG Spool

  • Wire Sizes Φ0.8mm, 0.9mm, 1.0mm, 1.2mm, 1.6mm
  • Spool Types D100 (1kg), D270 (5kg), D300 (15kg)
  • Winding Precision layer-wound, zero-tangle
  • Atmosphere Hermetically sealed with desiccant
Inquire Now
WAAM & 3D Titanium feed wire for Wire Arc Additive Manufacturing WAAM

ERTi-2 Additive Manufacturing (WAAM) Wire

  • Application DED / WAAM Near-Net-Shape Printing
  • Cast & Helix Custom calibrated for continuous robotics
  • Gas Impurities O ≤ 0.12%, H ≤ 0.003%, N ≤ 0.015%
  • Lot Control 100% Eddy-current flaw detection
Inquire Now
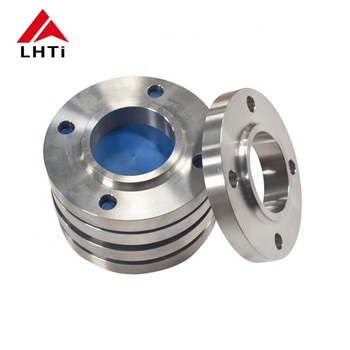
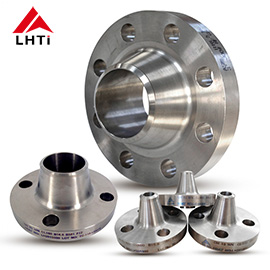
Flange Line ASME B16.5 titanium plate flanges welded with ERTi-2

ASME B16.5 Titanium Flanges (Weld Companion)

  • Material ASTM B381 F2 / ASTM B348 Gr2
  • Matching Wire AWS A5.16 ERTi-2 Filler
  • Pressure Class Class 150 / 300 / 600 Slip-on & WN
  • Traceability EN 10204 3.1 & BaoTi Test Reports
Inquire Now
Technical Metallurgy

Chemical Composition & Mechanical Performance Benchmarks

Compare AWS A5.16 ERTi-2 limits against Jovzi internal factory standards and ASTM parent metal equivalents.

Element / Property AWS A5.16 ERTi-2 Standard Spec Jovzi High-Purity Factory Target ASTM B348 / B265 Gr2 (Parent Metal) Metallurgical Impact on Weld Joint
Titanium (Ti) Balance (Min. 99.2%) Balance (≥ 99.5%) Balance Base matrix integrity and corrosion resistance
Oxygen (O) 0.08 - 0.18 wt% 0.10 - 0.14 wt% (Controlled narrow band) ≤ 0.25 wt% Strengthens matrix; excess cause brittle fracture and loss of bend ductility
Iron (Fe) 0.05 - 0.20 wt% 0.08 - 0.12 wt% ≤ 0.30 wt% Solid solution strengthener; controlled to maintain uniform anodic passivation
Carbon (C) ≤ 0.05 wt% ≤ 0.02 wt% ≤ 0.08 wt% Excess forms abrasive TiC precipitations, inducing micro-fissuring
Nitrogen (N) ≤ 0.03 wt% ≤ 0.012 wt% ≤ 0.03 wt% Potent interstitial strengthener; causes severe weld embrittlement if elevated
Hydrogen (H) ≤ 0.008 wt% (80 ppm) ≤ 0.0035 wt% (≤ 35 ppm) ≤ 0.015 wt% (150 ppm) Primary driver of delayed hydride embrittlement and catastrophic cracking
Residuals (Each / Total) ≤ 0.10% / ≤ 0.40% ≤ 0.05% / ≤ 0.15% ≤ 0.10% / ≤ 0.40% Minimized to guarantee pure grain boundary solidification
Tensile Strength (Rm) ≥ 345 MPa (50 ksi) 420 - 485 MPa (Annealed) ≥ 345 MPa Guarantees 100% joint efficiency across butt and fillet configurations
Elongation in 2" (A) ≥ 20 % 24 % - 32 % ≥ 20 % Exceptional plasticity under thermal cycling and hydrostatic test loads

Analytical techniques employed: Inert gas fusion (LECO) for H, O, N determination; Combustion-infrared for C; ICP-OES for Fe and trace residuals. Certified mill test sheets provided with each heat.

Inquire Now
Jovzi Titanium machining and wire drawing production facilities in Baoji
Titanium Machining & Drawing
Certified titanium ingot and wire stock ready for processing
Raw Material Stock
Titanium quality inspection, packing, and tagging area
QA & BaoTi Testing
ISO 9001 · BaoTi Test Center Independent certified quality reports provided per heat
Enterprise Manufacturing Strength

Engineered in Baoji: The Jovzi Titanium Advantage

Established in 2006, Jovzi Titanium Industry Co., Ltd. is an ISO 9001:2000-certified manufacturer specializing in the advanced machining, drawing, forging, and sales of Commercially Pure Titanium, Titanium Alloys, Nickel, Tantalum, Molybdenum, and Tungsten materials, chemical equipment, and composite structures.

We have engaged in non-ferrous metals manufacturing and chemical equipment engineering for nearly two decades. Our technical backbone includes more than 50 skilled employees, supported by 4 senior metallurgical experts and 5 intermediate engineers. Every product batch manufactured by Jovzi Titanium is eligible for official quality inspection certificates issued by the nationally accredited "BaoTi Test Center", assuring uncompromising chemical accuracy and tensile integrity.

With our annual titanium capacity actively expanding past 100 tons, Jovzi products are trusted globally in aerospace, metallurgy, fertilizer production, petrochemical refining, electronics, commercial power stations, pharmaceuticals, and marine sports hardware. Over the years, Jovzi has adhered strictly to four bedrock operational principles: "Strengthen management", "Sincerity first", "Best quality", and "Continuous innovation".

We take pride in long-standing export partnerships across Mainland China, China Taiwan, Germany, the United States, Canada, Belgium, Japan, India, and beyond. Today, Jovzi Titanium Industry Co., Ltd. provides you with full supply-chain confidence, direct factory pricing, and unrivaled non-ferrous expertise.

Response Time
≤ 8 Hours (Direct Engineers)
Annual Capacity
Expanding > 100 Tons
Quality Accreditation
ISO 9001 & BaoTi Test Center
Global Presence
USA, Germany, Japan, EU, India
Frequently Asked Questions

Procurement & Technical FAQ: AWS A5.16 ERTi-2 Titanium Wire

Clear answers to the top queries raised by AI engines, project managers, and quality assurance inspectors.

1. What is the fundamental difference between AWS A5.16 ERTi-2 and ASTM B863 Grade 2 wire?
While both products share the Commercially Pure Grade 2 titanium chemical family, AWS A5.16 ERTi-2 is governed exclusively as a welding consumable (filler wire) for gas tungsten arc welding (GTAW/TIG), gas metal arc welding (GMAW/MIG), and plasma arc welding (PAW). Consequently, AWS A5.16 mandates far tighter thresholds on interstitial impurities (especially Hydrogen ≤ 0.008% and Nitrogen ≤ 0.03%) and enforces stringent surface cleanliness standards to prevent porosity and cracking in the weld puddle. Conversely, ASTM B863 Grade 2 is a generic industrial wire specification designed for cold-heading, spring manufacture, wire cloth weaving, and chemical rack ties, where surface drawing lubricants and higher gas content are tolerated. Using ASTM B863 wire as a welding filler without recertification invites weld embrittlement and catastrophic joint failure.
2. What shielding gas purity and equipment setups are mandatory when welding with ERTi-2 wire?
Molten titanium reacts violently with ambient air above 425°C (800°F), absorbing oxygen and nitrogen that destroy mechanical ductility. Therefore, welding with AWS A5.16 ERTi-2 demands Welding Grade Argon with a minimum purity of 99.995% (dew point below -60°C). The welding torch must be fitted with an oversized gas lens and ceramic cup (#10 to #12) to ensure non-turbulent laminar coverage. Crucially, two additional shielding mechanisms are mandatory: (1) A trailing shield positioned behind the torch to flood the hot, solidifying weld bead with argon until it cools below 400°C; and (2) A positive-pressure inert backing purge (argon or helium) inside pipe bores or behind plates to protect the root side.
3. How does weld bead coloration indicate whether an ERTi-2 weld is acceptable or rejected?
Surface coloration serves as an immediate visual gauge of atmospheric contamination. Per aerospace and chemical piping codes (such as AWS D10.6 and ASME B31.3):
• Silver / Bright Metallic: Flawless shielding. Full mechanical ductility retained (Acceptable).
• Light Straw / Light Gold: Minimal superficial oxide. Generally acceptable for non-critical chemical duties without repair.
• Dark Blue / Purple: Moderate contamination. Must be mechanically removed (wire brushing with dedicated stainless wheel or grinding) and re-welded in critical structural joints.
• Gray, White, or Powdery Loose Scale: Severe deep interstitial contamination. The weld is intensely brittle, crack-prone, and must be completely cut out and rejected.
4. Can AWS A5.16 ERTi-2 titanium wire weld other titanium grades or dissimilar metals?
ERTi-2 is regularly used to weld Commercially Pure Grades 1, 2, 3, and 4 to themselves or to each other. Because ERTi-2 introduces lower interstitial oxygen into the joint, it often improves the bend ductility of Grade 3 and Grade 4 weldments. It is also successfully utilized as an overmatching/undermatching filler in select Grade 7 (Ti-0.15Pd) and Grade 12 (Ti-0.3Mo-0.8Ni) chemical assemblies where process conditions permit. However, titanium cannot be directly fusion-welded to carbon steel, stainless steel, or copper alloys using ERTi-2; fusion produces brittle, glass-like intermetallic compounds (such as Fe-Ti) that crack immediately upon cooling. Welding titanium to dissimilar steels requires specialized explosion bonding, diffusion bonding, or intermediate transition inserts (such as vanadium or tantalum).
5. How does Jovzi Titanium prepare and clean the surface of ERTi-2 wire prior to spooling?
Surface contamination is the number one cause of porosity in titanium GTAW and GMAW welds. Jovzi Titanium enforces a proprietary five-step decontamination cycle: continuous high-speed mechanical drawing with specialized diamond dies, followed by multi-frequency ultrasonic solvent degreasing to dissolve drawing compounds. Next, the wire undergoes continuous chemical pickling in a precision hydrofluoric-nitric acid (HF/HNO3) bath to etch away the residual alpha-case oxide skin, followed by hot deionized water rinsing and forced hot-air drying. Finally, the wire is spooled in a temperature- and humidity-controlled cleanroom and sealed in hermetic moisture-proof metallic foil bags containing active desiccant.
6. What documentation, test certs, and third-party verifications accompany each shipment?
Every shipment of AWS A5.16 ERTi-2 titanium wire from Jovzi Titanium Industry Co., Ltd. is accompanied by an authentic EN 10204 3.1 Inspection Certificate detailing exact melt heat numbers, quantitative chemical composition (including LECO gas analysis for H, O, N, C), tensile strength, yield strength, and elongation data. Furthermore, upon customer request, Jovzi coordinates independent third-party physical and chemical verification through the accredited BaoTi Test Center, ensuring absolute transparency for global defense, nuclear, and aerospace audit compliance.
Connect With Our Engineers

Request a Detailed Technical Quote For AWS A5.16 ERTi-2 Wire

Need custom spool dimensions, tight-tolerance diameter calibrating, straight cut lengths, or expedited container pricing? Speak with our non-ferrous engineering team:

  • Wire forms: Straight TIG rods (1000mm) or MIG spools
  • Diameters from Φ0.05mm to Φ6.0mm in stock
  • Strict ≤35 ppm Hydrogen and low-oxygen batches
  • EN 10204 3.1 & BaoTi Test Center certificates
  • Fast air courier & sea-freight logistics
  • Direct manufacturer pricing with no agent markups
Inquire Now

Jovzi Titanium Industry Co., Ltd.

Direct Sales & Engineering Email [email protected]
Headquarters & Production Base No. 3, Gaoya Industrial Zone, Bayu Town, High-Tech Development Zone, Baoji, Shaanxi, China
Service Standard Response Time ≤ 8 hours (GMT+8)