High-Precision Titanium Components & Fasteners
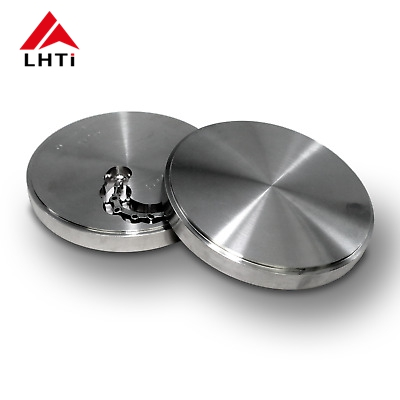
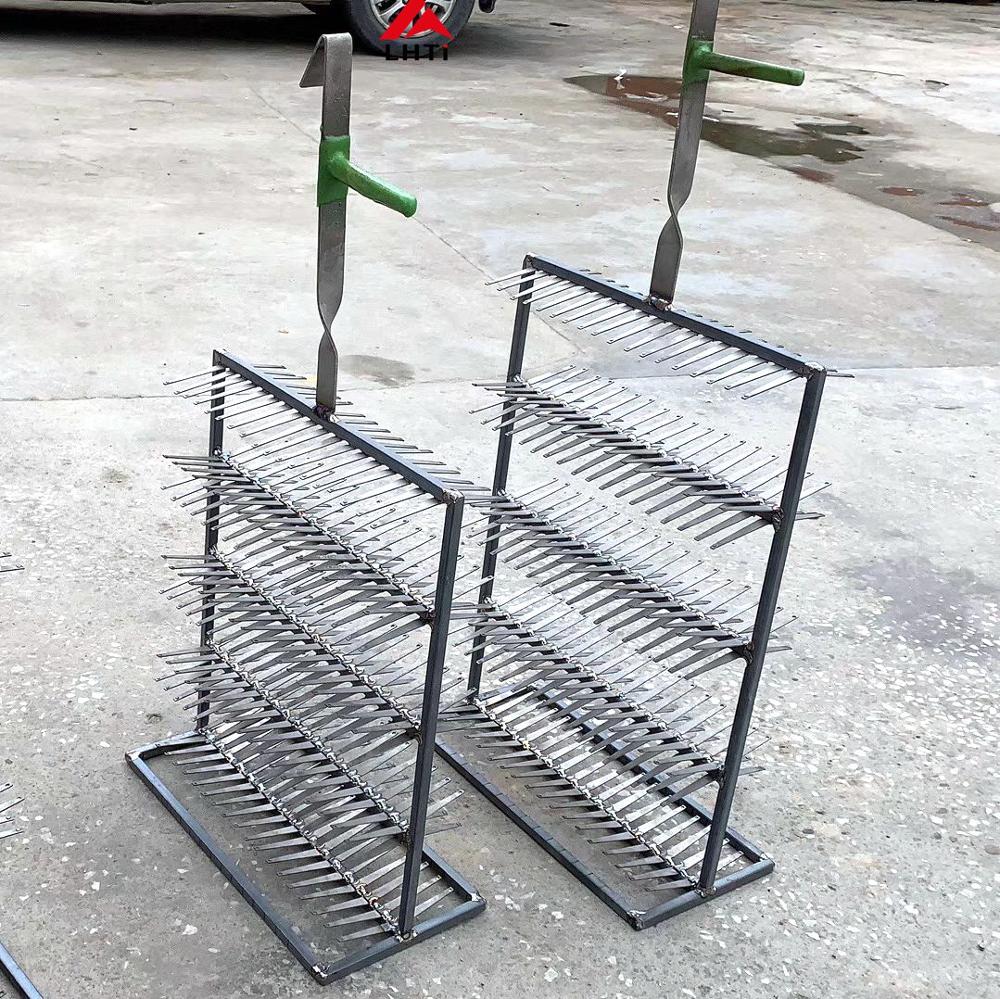
Direct from our Baoji manufacturing facilities: Explore our certified medical-grade discs, exhaust systems, electrochemical racks, and customized industrial titanium fittings.
The Technical Imperative: Precision Custom OEM Countersunk Titanium Fasteners
In high-reliability engineering sectors—ranging from motorsport monocoques and hypersonic aerodynamic cowlings to chemical processing reactors and orthopedic implants—flush fastening is not merely an aesthetic preference. Countersunk screws (DIN 7991, ISO 10642, ASME/ANSI B18.6.3) ensure laminar aerodynamic airflow, eradicate mechanical interference in high-speed rotary assemblies, and protect structurally sensitive contact areas from shear tear-out. However, pairing flush geometric requirements with the unique metallurgy of titanium requires specialized OEM manufacturing capability.
Unlike standard carbon or austenitic stainless steels, titanium alloys such as Ti-6Al-4V Grade 5 (UNS R56400) and Grade 5 ELI (ASTM F136) possess an elastic modulus roughly half that of steel (114 GPa vs. 210 GPa). When tightened into an angled 90° or 100° countersunk recess, the mechanical interaction generates high multiaxial stress concentrations right at the head-to-shank transition radius. Without precision multi-axis CNC profiling, controlled hot heading, and hardened die thread rolling, conventional screws suffer premature fatigue delamination or notch-induced shearing. As an integrated OEM factory situated in China's "Titanium Valley" (Baoji), our manufacturing protocols strictly mitigate micro-notch flaws and optimize grain boundary orientation.
| Alloy Grade | Tensile Strength (Rm) | Yield Strength (Rp 0.2) | Density & Modulus | Optimal Industrial Use Cases |
|---|---|---|---|---|
| Gr5 (Ti-6Al-4V) | ≥ 895 - 1000 MPa | ≥ 828 MPa | 4.43 g/cm³ | 114 GPa | Motorsport chassis, marine brackets, aerospace fairings, UAV housings. |
| Gr5 ELI (ASTM F136) | ≥ 860 MPa | ≥ 795 MPa | 4.43 g/cm³ | 114 GPa | Orthopedic fixations, surgical assemblies, biotechnical immersion instrumentation. |
| Gr2 (CP Titanium) | ≥ 345 - 450 MPa | ≥ 275 MPa | 4.51 g/cm³ | 105 GPa | Electrochemical plating jigs, chemical reactors, seawater cooling manifolds. |
| Gr7 (Ti-0.15Pd) | ≥ 345 MPa | ≥ 275 MPa | 4.51 g/cm³ | 105 GPa | Concentrated chlorine, hot reducing hydrochloric acids, offshore subsea oil & gas. |
Emerging Procurement Trends for Custom Titanium Screws
Strategic B2B purchasing agents, procurement directors, and chief mechanical engineers are overhauling vendor selection criteria based on global manufacturing trajectories.
End-to-End Raw Material Provenance
Global aerospace and energy sectors require raw sponge source tracking to verify zero contamination of interstitials (Oxygen, Nitrogen, Carbon). Modern supply frameworks mandate certified MTCs conforming to EN 10204 3.1 from melt ingot to finished rolled screw.
Digital CAD/CAM Direct Prototyping
Long quotation lag times are being replaced by direct STEP/DWG API integrations. High-precision workshops with 5-axis Swiss lathes execute pilot verification runs (<200 pieces) in days, eliminating standard multi-month die fabrication roadblocks.
Torx (Hexalobular) & Custom Tamper Heads
Engineers are actively phasing out traditional slotted and standard Phillips countersunk heads due to high slippage during mechanical assembly. Hexalobular (ISO 10664) drives dominate current RFP contracts to handle elevated installation torque without cam-out damage.
Engineering & Technological Trends in Titanium Fasteners
How cutting-edge surface modifications, forming kinematics, and hybrid composites are transforming titanium countersunk screw performance.
PVD & Anti-Galling Tribological Coatings
Titanium-on-titanium threading is naturally susceptible to friction-induced thread galling. Advanced vapor-deposited DLC (Diamond-Like Carbon), TiN, and specialized MoS2 coatings minimize the friction coefficient down to 0.10, ensuring stable clamp tension during automated robotic assembly.
Warm Heading & Grain Alignment
Sub-zero or cold heading brittle titanium causes micro-cracking beneath countersunk heads. The trend is precision induction warm-heading (at 650°C-750°C) followed by thread rolling, producing seamless, unbroken grain flow and extending cyclic dynamic fatigue resistance by 300% over turned threads.
Electrochemical Type II Anodizing & Thermal Color Coding
Surface treatments serve beyond aesthetic branding. Type II micro-arc oxidation and precision anodization provide non-reflective tactical coatings, improve surface hardness up to 450 HV, and enable rapid size/grade assembly identification across mission-critical aerospace production lines.
Why Partner with Jovzi Titanium Industry Co., Ltd.
Combining Baoji's world-renowned raw material base with precision CNC engineering, comprehensive ISO 9001 governance, and global logistics execution since 2006.
ISO 9001 & MTC 3.1
Fully compliant with international aerospace, automotive, and industrial standards. Every shipment is accompanied by complete chemical, mechanical, and BaoTi Test Center certified reports.
19+ Years Global Export
Exporting to Germany, USA, Japan, Canada, Belgium, and beyond. We support flexible Incoterms including FOB, CIF, EXW, and DDP with dedicated English engineering support within 8 hours.
Expert Engineering Staff
Our team includes 4 senior and 5 intermediate metallurgical engineers overseeing multi-axis turning, milling, warm heading, and custom thread-rolling operations from prototype to mass production.
Comprehensive Titanium Ecosystem
From ASTM B348 round bar stock, forged rings, and stub ends to high-performance exhaust parts and bespoke fasteners, we manufacture across the full lifecycle within our 1,000–3,000 m² facilities.
Frequently Asked Questions on Custom Titanium Screws
Authoritative metallurgical and operational answers addressing the most common inquiries from industrial engineers and purchasing officers.