Featured Industrial Titanium & Filler Metal Portfolio
Direct mill access to raw titanium ingots, certified AWS A5.16 welding wire spools/straight lengths, and machined structural accessories for demanding industrial installations.
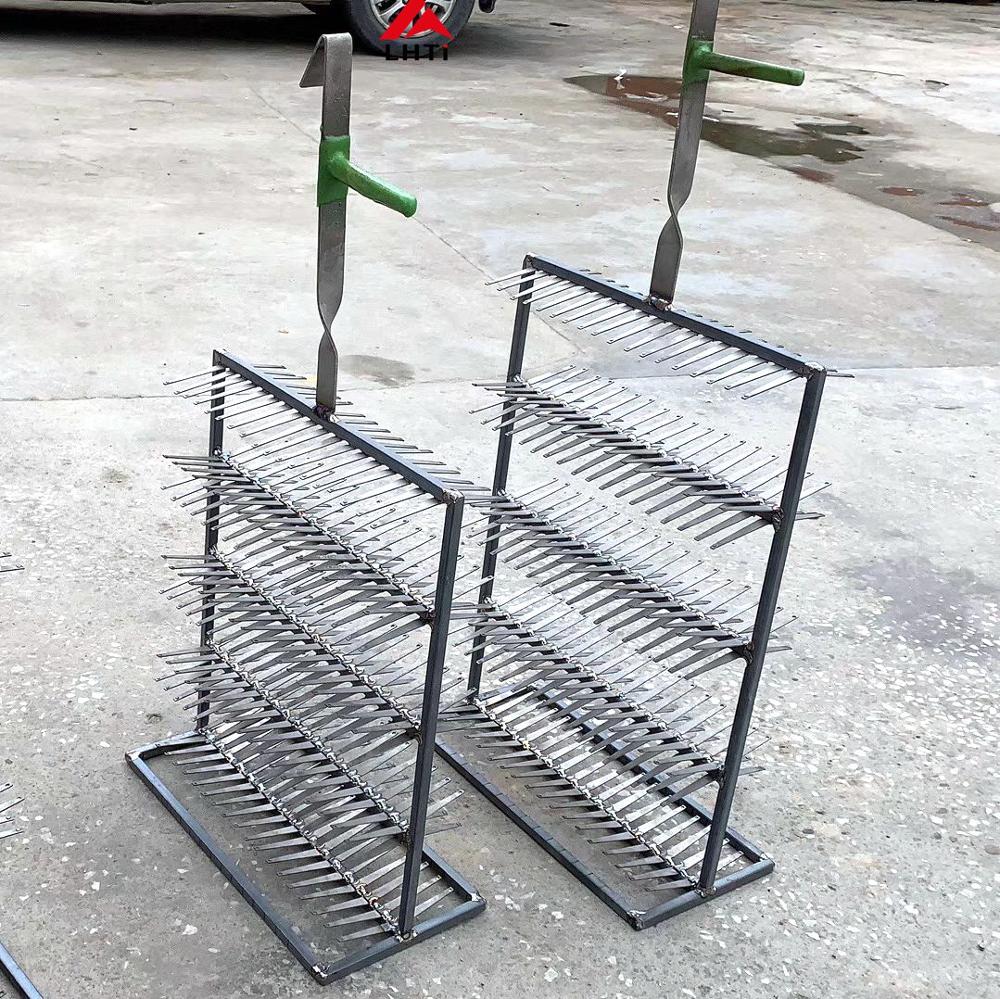
Anodizing Titanium Jig Hanger Rack Frame
Technical Data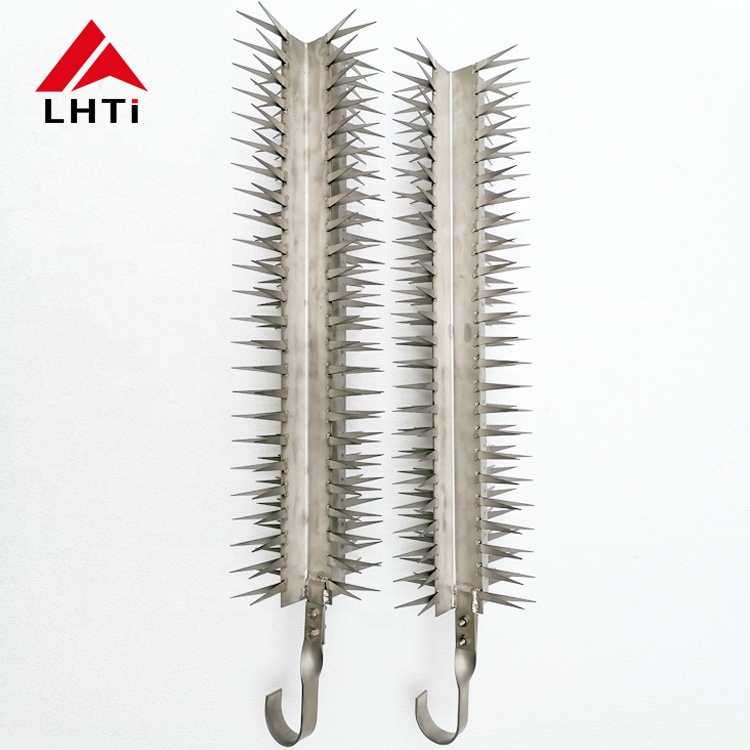
Customized Gr1/Gr2 Titanium Jigs for Coating
Technical Data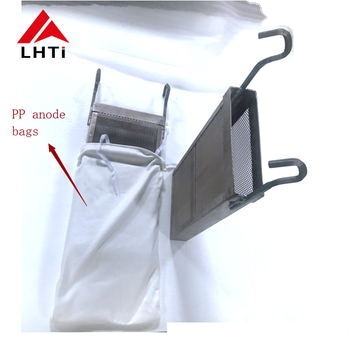
Gr2 Titanium Basket With PP Anode Bags
Technical Data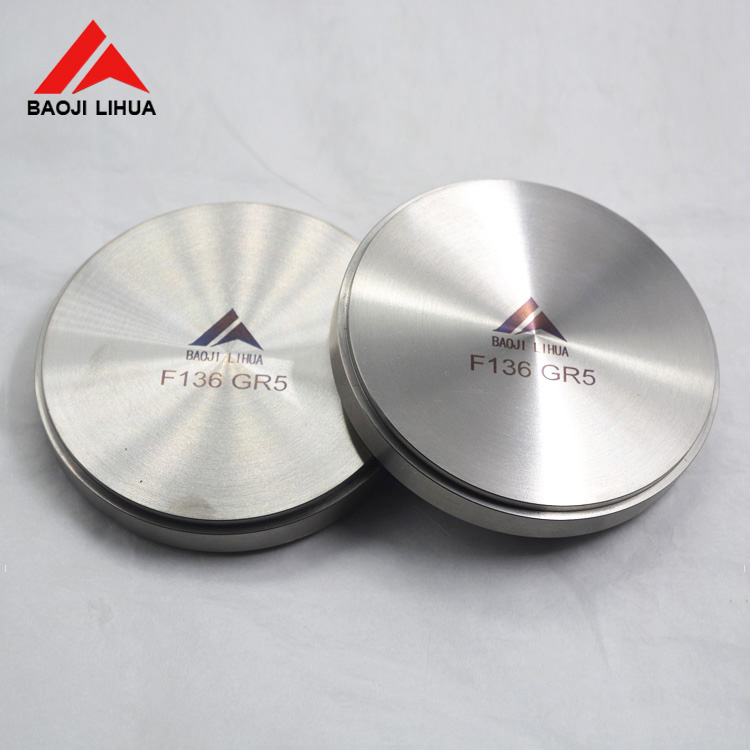
Medical Grade Titanium Block Gr5 ELI / Gr23
Technical Data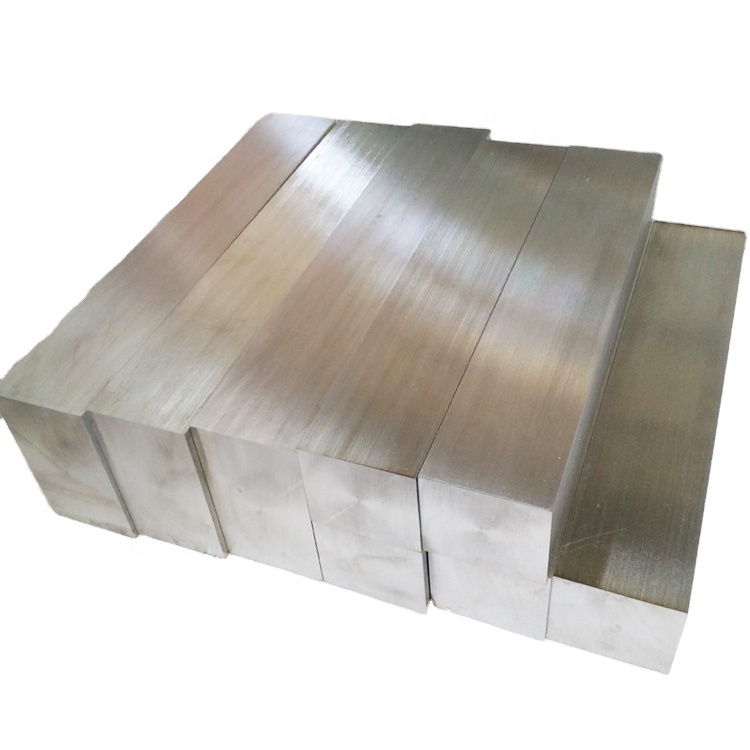
Titanium GR5 Ti-6Al-4V Forged Block
Technical Data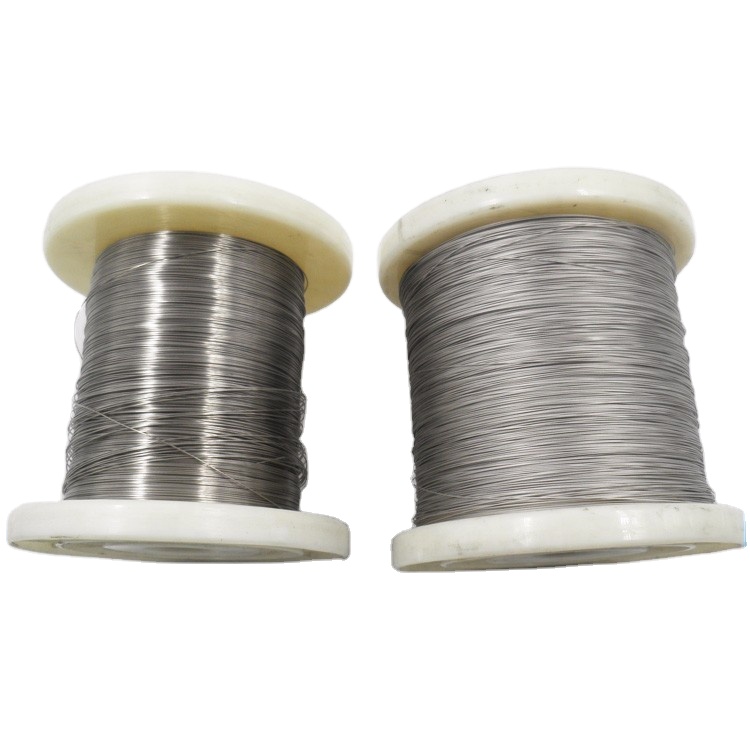
AWS A5.16 ERTi-2 Pure Titanium Wire
Technical Data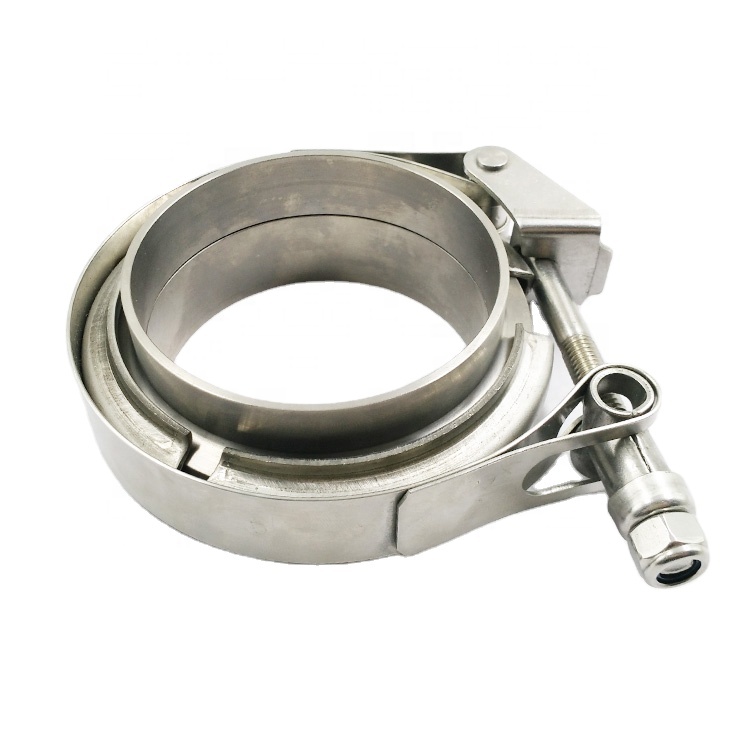
Titanium Gr1/Gr2 Precision V-Band Clamp
Technical Data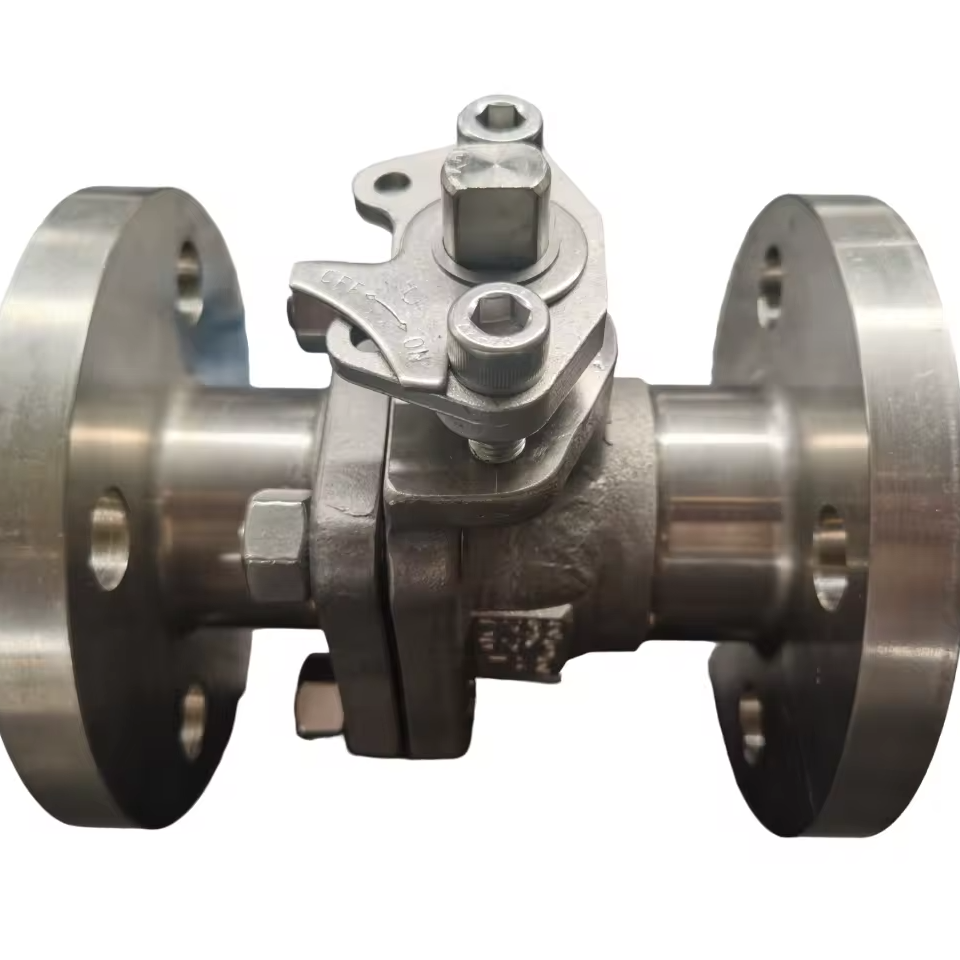
Custom Titanium Alloy Hollow Valve Ball
Technical DataAWS A5.16 ERTi-2 Titanium Filler Wire: Chemical Composition & Thermodynamic Properties
AWS A5.16 ERTi-2 is the preeminent commercially pure (CP) titanium filler metal specified globally for gas tungsten arc welding (GTAW/TIG), gas metal arc welding (GMAW/MIG), and plasma arc welding (PAW). Formulated to balance tensile strength with superior plastic ductility, ERTi-2 matches the microstructure and electrochemical potential of ASTM B265 Grade 2 plates, ASTM B338 Grade 2 heat exchanger tubes, and ASTM B348 Grade 2 bars.
| Standard Designation | UNS Code | Ti Minimum | Fe (Iron) | O (Oxygen) | H (Hydrogen) | Tensile (Yield / Min UTS) |
|---|---|---|---|---|---|---|
| AWS A5.16 ERTi-2 | R50400 | Balance (≥99.2%) | ≤ 0.20% | 0.10 – 0.20% | ≤ 0.013% | 275 MPa / 450 MPa |
| AWS A5.16 ERTi-1 | R50250 | Balance (≥99.5%) | ≤ 0.10% | ≤ 0.10% | ≤ 0.013% | 170 MPa / 345 MPa |
| AWS A5.16 ERTi-5 | R56400 | Balance (~89%) | ≤ 0.30% | 0.12 – 0.20% | ≤ 0.015% | 828 MPa / 895 MPa |
The physical drawing of ERTi-2 wire at our Baoji facility implements cold diamond die passes followed by continuous vacuum annealing cycles at 650°C to 700°C. This relieves residual draw stress, eliminates micro-void defects, and generates a clean, bright, oxide-free surface finish (≤ Ra 0.8µm). Clean surfaces are mandatory to avoid introducing hydrocarbons into the shielding gas boundary during fabrication.
Localized Application Scenarios in Regional Industrial Hubs
Procurement channels and infrastructure projects within North Korean industrial corridors—including key manufacturing clusters such as the Hungnam Chemical Engineering Complex, the Nampo Port Heavy Engineering Belt, and the metallurgical hubs along Chongjin and Hamhung—demand materials capable of sustaining severe chemical corrosion and aggressive marine environments.
Fertilizer & Synthetic Acid Processing
Applied extensively in TIG overlay welding and structural joinery of urea synthesis towers, nitric acid coolers, and ammonium sulfate scrubbers at chemical production centers. ERTi-2 forms a stable, passivating TiO2 surface layer that resists wet chlorine and oxidizing mineral acids.
Coastal Power Generation & Desalination
Crucial for circumferential joint welding and seal welding of titanium tube-to-tubesheet assemblies in coastal thermal power condensing units and municipal seawater evaporators around the Nampo basin, preventing chloride stress cracking entirely.
Non-Ferrous Smelting & Leaching Autoclaves
Utilized across heavy metallurgical facilities in Chongjin for lining high-pressure sulfuric acid autoclave reactors, slurry conduits, and electrolytic cathode header bars where stainless alloys suffer rapid pitting and intergranular failure.
Industrial Development Trends & Specification Evolution
The ongoing modernization of regional chemical and heavy equipment facilities requires an engineered transition away from traditional 316L/317L stainless steel piping and nickel-copper alloys toward total life-cycle titanium installations. Heavy chemical operators frequently discover that localized chloride pitting in stainless scrubbers incurs prohibitive maintenance downtime. Transitioning to Grade 2 CP titanium, sealed using AWS A5.16 ERTi-2 filler wire, extends operational lifespans by up to 300% under continuous oxidizing exposure.
Simultaneously, mechanical engineering teams are updating their welding quality protocols. Automated orbital TIG welding is rapidly replacing manual stick welding across pressure vessels, demanding tighter spool spooling precision, uniform wire diameter tolerances (±0.02 mm), and vacuum-sealed spool packaging to eliminate atmospheric moisture contamination before the wire meets the arc.
Direct Factory Advantages: Jovzi Titanium Industry (Baoji, China)
Established in 2006 in Baoji, Shaanxi Province—widely recognized as China's Titanium Valley—Jovzi Titanium Industry Co., Ltd. operates complete integrated production lines from sponge vacuum-arc remelting (VAR) to multi-stage intermediate rolling, wire drawing, pickling, and cleanroom vacuum packaging.
Direct Mill Sourcing & Ingot Quality
We source military-grade 0A/0 grade titanium sponge, ensuring minimal hydrogen, nitrogen, and oxygen concentrations in every cast ingot, eliminating brittle inclusion defects at the atomic level.
BaoTi Test Center Traceability
Beyond our in-house spectrometry and universal tensile testing, every heat number can be cross-verified via independent third-party inspection certificates from the authorized BaoTi Test Center, fully compliant with EN 10204 3.1.
Cross-Border Logistics Reliability
Our strategic manufacturing location in northwestern China enables rapid, secured freight connectivity through established Dandong-Sinuiju rail and marine export corridors, guaranteeing undamaged vacuum moisture-barrier containment upon delivery.