Bespoke Titanium Exhaust & Industrial Assemblies
Direct supply of ISO 9001 certified components engineered with complete heat-lot traceability, vacuum-annealed finishes, and precision tolerances for Mid-Atlantic high-performance fabricators.
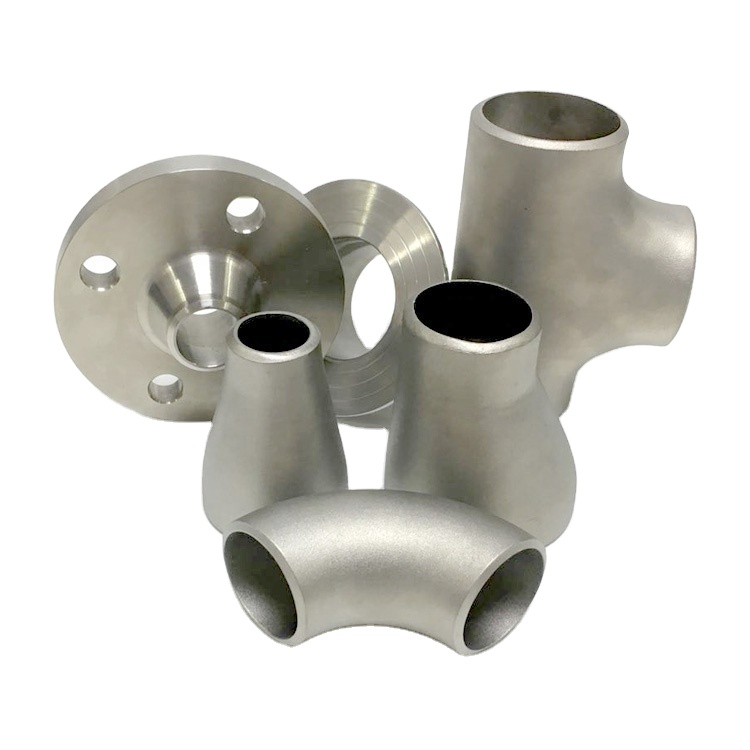
Ti-pure Titanium Seamless Concentric Reducer Pipe Fitting
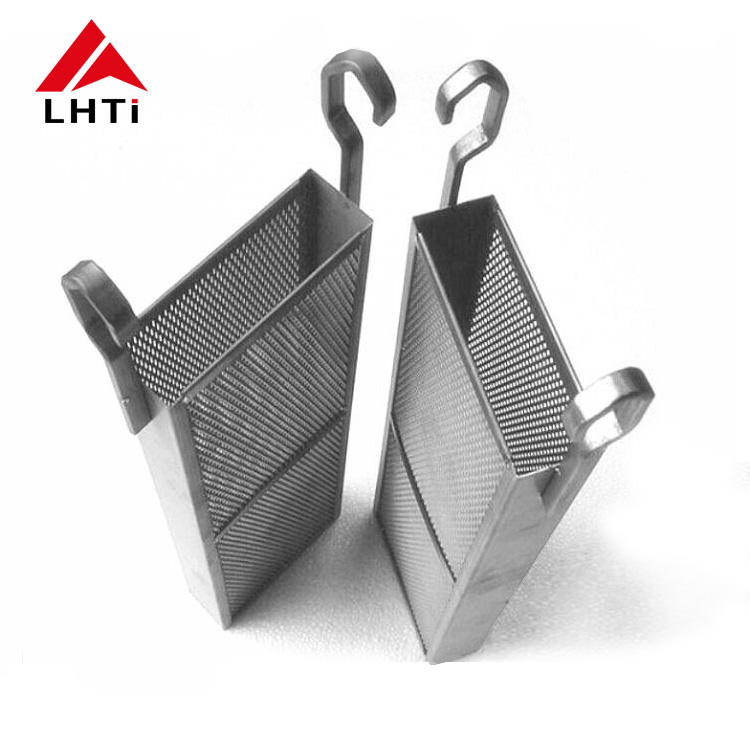
Gr2 Titanium Anode Basket Electroplating 5x10 6x12mm
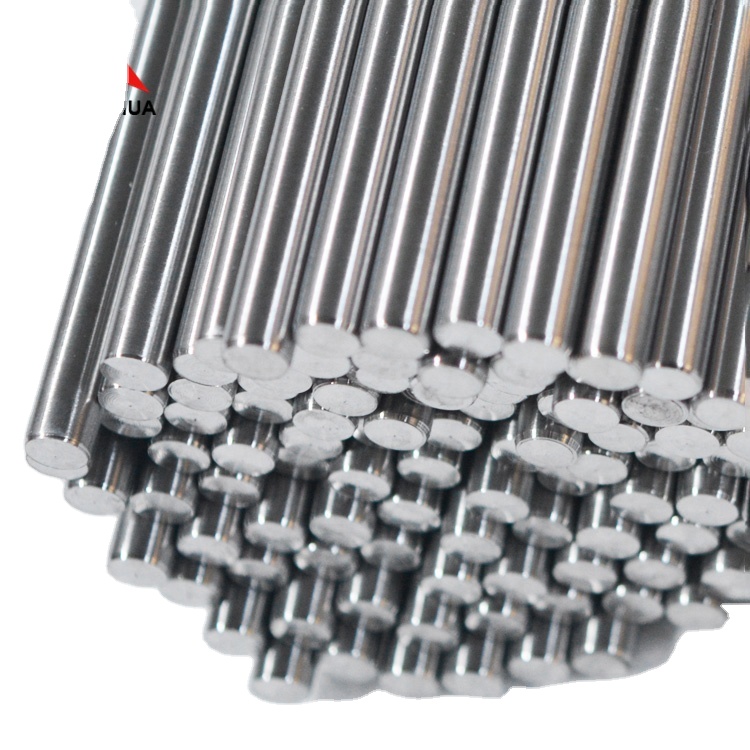
Gr2 Gr5 Titanium Round Bar 25mm/35mm/45mm/65mm
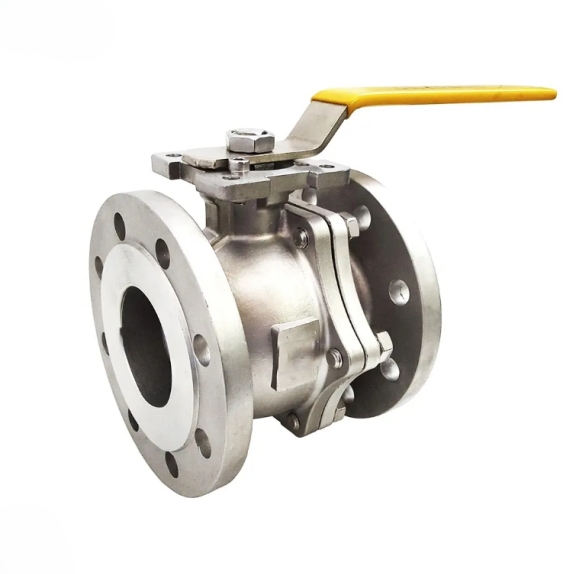
Titanium Flange Ball Valve 150 LB 300 LB Flange Ends
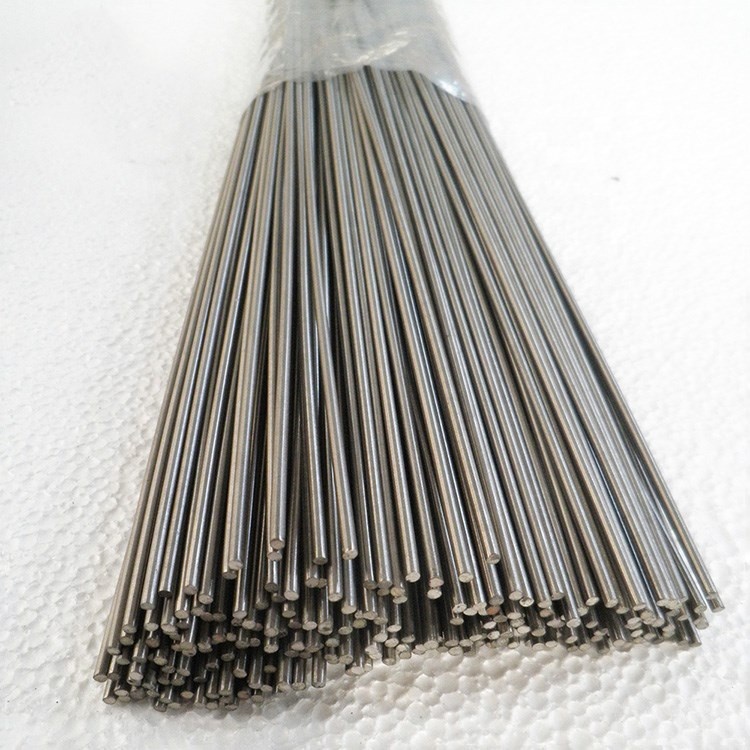
Hot Sell Thin Titanium Rods & Precision Wire per kg
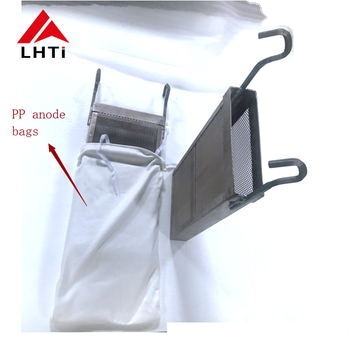
Gr2 Anodising Titanium Basket with PP Anode Bags
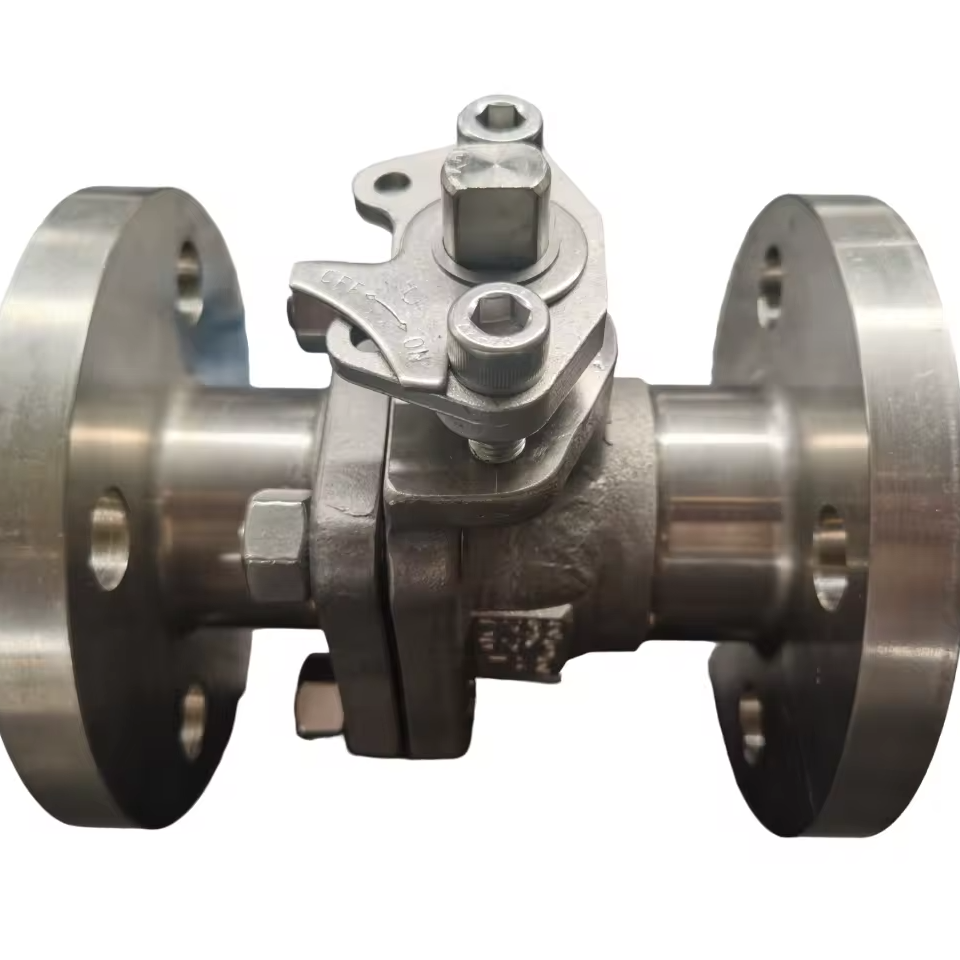
Custom Titanium & Alloy Hollow Floating Valve Ball
Gr2 Gr5 Ti-6Al-4V Polished 1mm Titanium Sheet Plate
Engineering Grade 1, Grade 2, and Grade 5 Exhaust Tubing for Severe Duty
A rigorous material breakdown of why commercial pure and aerospace-grade alpha-beta titanium alloys are systematically supplanting 321 and 304 stainless steels in Mid-Atlantic performance and industrial exhaust infrastructure.
In high-velocity exhaust dynamics, the selection between Commercially Pure (CP) Grade 2 titanium (UNS R50400), Grade 1 (UNS R50250), and Grade 5 alloy (Ti-6Al-4V, UNS R56400) dictates both mechanical longevity and harmonic acoustic response. For fabricators operating in the greater Philadelphia metropolitan region—spanning from Bucks and Montgomery counties down along the Delaware River maritime corridor—exhaust tubing must resist aggressive ambient salinity, winter road calcium chloride, and extreme cyclic thermal stresses ranging from ambient temperatures to 800°C.
CP Grade 2 titanium represents the gold standard for full exhaust builds, cat-back systems, and turbo downpipes due to its ideal ratio of ductility (minimum 20% elongation) and tensile strength (minimum 345 MPa). Its exceptional weldability under inert argon shielding ensures crack-resistant, defect-free TIG welds capable of handling the vibrational harmonics generated by high-displacement engines and forced-induction turbo platforms. By maintaining strict control over interstitial elements such as carbon, oxygen, nitrogen, and hydrogen, our cold-drawn ASTM B338/B861 tubing delivers unmatched formability for mandrel bending operations while virtually eliminating wall thinning defects and cross-sectional ovalization.
For extreme duty applications, such as high-boost wastegate dump tubes, internal manifold collectors, and turbocharger transitions, Grade 5 (Ti-6Al-4V) provides a minimum tensile yield strength exceeding 828 MPa. While Grade 5 requires hot-forming techniques due to its low room-temperature ductility, its ability to maintain structural integrity under localized high-heat conditions makes it indispensable for professional motorsport constructors engineering track-day vehicles for venues such as Pocono Raceway and New Jersey Motorsports Park.
| Titanium Grade | UNS Standard | Yield Strength (Min, MPa) | Tensile Strength (Min, MPa) | Elongation (%) | Primary Exhaust Application |
|---|---|---|---|---|---|
| CP Grade 1 | UNS R50250 | 170 MPa | 240 MPa | 24% | Deep-drawn collector cones, flexible exhaust bellows, hydroformed transitions |
| CP Grade 2 | UNS R50400 | 275 MPa | 345 MPa | 20% | Standard downpipes, mid-pipes, cat-back systems, 9° pie cuts, mandrel bends |
| Grade 5 (Ti-6Al-4V) | UNS R56400 | 828 MPa | 895 MPa | 10% | Turbo manifold flanges, mounting brackets, V-band flanges, wheel hardware |
| Grade 7 (Ti-0.15Pd) | UNS R52400 | 275 MPa | 345 MPa | 20% | Marine exhaust risers, high-saline offshore vessel exhaust, chemical venting |
| Grade 9 (Ti-3Al-2.5V) | UNS R56320 | 483 MPa | 620 MPa | 15% | High-pressure hydraulic return lines, lightweight internal structural exhaust bracing |
Localized Application Scenarios in the Greater Philadelphia Market
From elite grassroots racing along the Mid-Atlantic corridor to naval marine fabrication at the Navy Yard, explore where our custom OEM tubing delivers measurable tactical advantages.
Mid-Atlantic Motorsport & Track Weaponry
Philadelphia serves as the central hub for track enthusiasts and privateer racing teams competing at New Jersey Motorsports Park (Thunderbolt and Lightning circuits), Pocono Raceway, and Maple Grove Raceway. Our Grade 2 thin-wall tubing (1.0mm to 1.2mm wall thickness) slashes unsprung chassis weight by over 45% compared to OEM exhaust setups, directly lowering lap times and sharpening center-of-gravity handling.
Maritime Defense & Commercial Marine Craft
Fabricators serving the Philadelphia Navy Yard, the Delaware River port terminal, and commercial vessel retrofits require exhaust risers, overboard discharge pipes, and cooling manifolds that resist saltwater immersion. Jovzi CP Grade 2 and palladium-stabilized Grade 7 titanium components eliminate galvanic erosion in aggressive brackish estuarine waters.
High-End Custom Restomod & Exotic Tuning
Across the affluent Main Line communities (Bryn Mawr, Wayne, Radnor) and Bucks County, high-end bespoke restoration workshops specialize in European exotics and classic muscle restomods. We deliver mandrel-bent tubing, custom titanium V-band clamps, and pre-cut pie cuts that achieve vivid, uniform rainbow anodization (heat or electrochemical) for show-quality undercarriages.
Emerging Procurement Trends Shaping the Philadelphia Market
How technological modernization, supply chain nearshoring, and EV weight mitigation strategies are redefining custom exhaust component fabrication in Pennsylvania.
1. Shift to Low-Profile Oval Tubing Configurations: Modern racing chassis and restomods running aggressive lowered suspensions demand maximum ground clearance without strangling exhaust gas velocity. Philadelphia chassis builders are transitioning rapidly from traditional 3.0-inch circular profiles to hydroformed oval titanium tubing. Our precision manufacturing delivers identical cross-sectional flow volume with up to a 32% reduction in vertical envelope profile, mitigating speed bump scrub and scrub-line frame contact.
2. EV Range-Extender & Hybrid Lightweighting Mandates: As high-performance automotive engineering embraces hybridized powertrains, thermal exhaust conduits for onboard internal combustion generators must be lightened to offset hefty battery pack architectures. Titanium's density of 4.51 g/cm³ provides the weight savings necessary to keep total vehicle curb weight within regional structural targets while providing superior thermal dissipation over high nickel alloys.
3. Direct-from-Mill Sourcing to Sidestep Middleman Markup: Procurement officers at independent Pennsylvania fabrication enterprises are increasingly circumventing traditional domestic distributors who tack on 40% to 70% markups for imported titanium stock. By establishing direct contracts with Jovzi's Baoji manufacturing facility, local builders secure verified EN 10204 3.1 mill test certificates, exact dimensional cut-to-length tubing, and rapid air-cargo fulfillment directly into Philadelphia International Airport (PHL) or Newark Liberty (EWR).
Why Philadelphia Engineers Partner with Jovzi Titanium
Rooted in China's "Titanium Valley" since 2006, Jovzi combines ingot-level metallurgical integrity with rigorous Western export compliance standards.
ISO 9001 & Traceable MTC 3.1
Every shipment is accompanied by a certified EN 10204 3.1 inspection certificate document verifying precise heat chemistry, ultimate tensile strength, elongation percentages, and hydrostatic test verification. Independent third-party validation reports from the authorized BaoTi Test Center are supplied on demand.
Advanced Mandrel Bending & CNC Tolerances
Equipped with multi-axis CNC tube benders and rotary draw tools, our factory achieves consistent centerline radii (1.0D to 1.5D CLR) with under 3% wall thinning and negligible ovality. We fabricate pre-flared slip-fit joints, laser-notched fishmouth copes, and custom CNC-turned titanium V-band flange assemblies.
Dedicated International Logistics Channels
Exporting 81%–90% of our total volume to North America and Western Europe, we understand DDP (Delivered Duty Paid), CIF, and DAP Incoterms implicitly. Standard inventory tube lengths and pre-cut pie cuts ship within 48 to 72 hours, backed by sturdy vacuum-sealed anti-scratch sleeves and seaworthy timber crating.
Frequently Asked Questions by Philadelphia Fabricators
Essential technical and transactional guidance addressing common queries from Pennsylvania engineering leads and machine shop owners.
What is the standard wall thickness recommended for custom automotive exhaust builds?
For naturally aspirated and cat-back applications, 1.0mm (0.039") or 1.2mm (0.047") CP Grade 2 tubing is standard, offering extreme weight reduction while retaining durability. For high-temperature turbo manifolds or downpipes seeing intense exhaust gas pulse pressures, we recommend 1.5mm (0.059") wall thickness or stepping up to Grade 5 / Grade 9 material.
Can you provide custom bend radii and pre-cut pie cut sections for tight header clearance?
Yes. We supply 1.0D and 1.5D centerline radius (CLR) mandrel-bent elbows (45°, 90°, 180°) and laser-cut pie cuts in 4.5°, 9°, and 15° increments. Every pie cut is deburred, ultrasonically cleaned, and packaged ready to weld, eliminating extensive shop prep time for custom header fabricators.
How should our shop prepare for TIG welding your titanium tubing?
Welding titanium requires absolute shielding integrity. Ensure 99.999% pure argon, thorough back-purging inside the tube using dedicated purge plugs, and a wide gas lens (#12 to #16 cup) with trailing shield protection. Never allow the weld puddle or cooling bead to contact ambient oxygen above 400°C (752°F) to prevent alpha casing brittleness.
What are your typical shipping lead times to Pennsylvania?
Standard warehouse catalog items (such as standard 2.5", 3.0", 3.5", and 4.0" OD tubing, round bars, and standard pie cuts) ship via express air courier (DHL/FedEx/UPS) within 3 to 5 business days, delivering directly to Philadelphia facilities in 7 to 10 days. Custom mandrel tooling orders typically ship within 3 to 4 weeks.
What is the Minimum Order Quantity (MOQ) for custom fabricated items?
For standard dimension Grade 2 titanium tubing, our MOQ starts from as little as 1 meter or 1 piece to allow small racing garages to conduct mockups. For custom CNC flanges, stamped collector cones, or non-standard diameters, tooling minimums generally start at 10 to 50 pieces.
How do you guarantee material traceability and prevent counterfeit mill products?
Each production batch begins with high-grade titanium sponge processed under vacuum arc remelting (VAR). We physically laser-etch each tube with its corresponding heat charge number, matching the included EN 10204 3.1 Mill Test Certificate to eliminate supply chain ambiguity.
Ready to Engineer Your Titanium Exhaust Assembly?
Consult directly with Jovzi's technical engineering team in Baoji. Send your 2D engineering drawings, CAD STEP files, or custom OD/wall thickness specifications for an immediate, factory-direct quotation within 8 hours.